Custom Natural Midnight Black Split Face Ledger Panels Exporter - Bulk Supply and Specification Guide
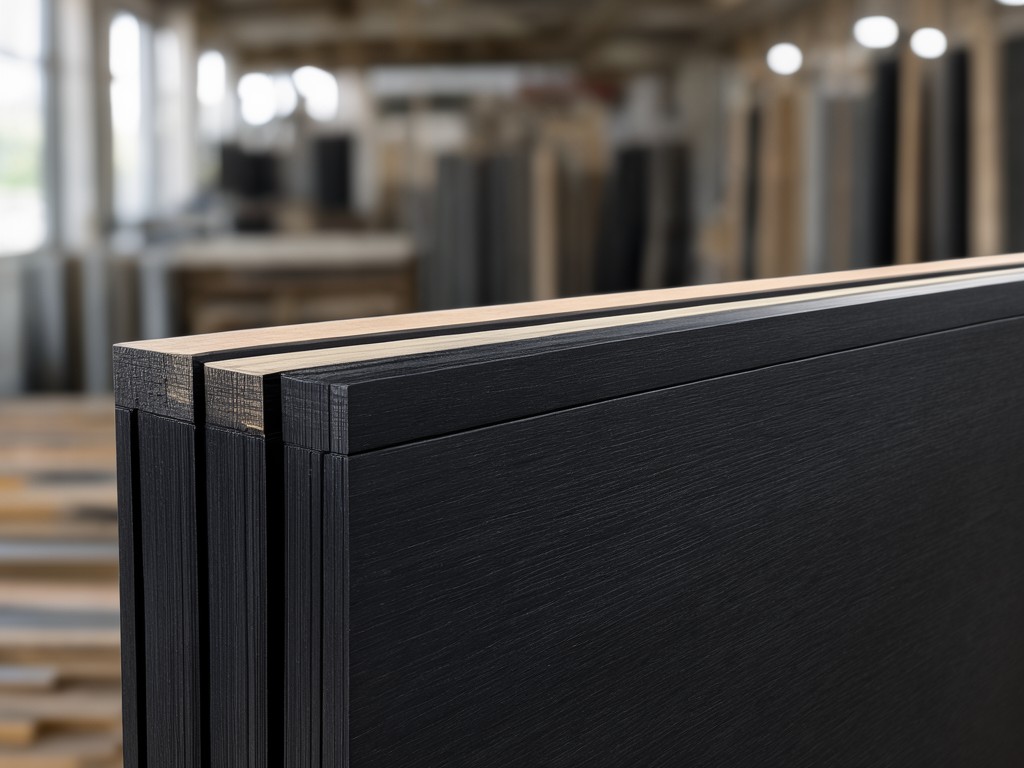
Structural integrity in formwork systems depends on the density of the core material and the precision of the surface finish. Split face ledger panels utilize a high-density engineered composite designed to resist the hydrostatic pressure of wet concrete without deforming over high-cycle use. The natural midnight black finish is applied via a vacuum-impregnated process that ensures the pigment does not delaminate under repeated mechanical impact or alkaline chemical exposure.
What This Is and Where It Fits
Procurement officers select these panels for high-rise structural elements where the concrete surface finish is a primary architectural requirement. The split face geometry provides a textured, non-porous bond that eliminates the need for secondary post-processing of the masonry. The midnight black coating is not merely aesthetic; it serves as a sacrificial layer against UV-induced degradation and mechanical abrasion during transport and installation.
- Load-bearing wall systems requiring high-tolerance-repeat concrete finishes.
- Optimized for precast element manufacturing where rapid stripping times are critical for throughput.
- Suitable for industrial infrastructure projects exposed to high-humidity and chemical de-icing agents.
Comparing Two Configurations
| Parameter | Standard Midnight Grade | Heavy-Duty Reinforced Grade |
|---|---|---|
| Cycle Life Rating | 50-75 cycles | 150+ cycles |
| Core Thickness | 18mm | 25mm |
| Surface Hardness | Standard Shore D Rating | High-Impact Polymer |
What Can Be Customised and What Cannot
Customization is focused on the physical dimensions and the integration of hardware to match existing onsite formwork systems. However, the core chemical composition of the midnight black split-layer remains fixed to ensure consistent structural load-bearing properties across the entire export batch.
Customizable Elements
- Custom panel lengths and widths (to ±2mm tolerance).
- Integrated tie-pocket configurations for specific bolt-rod systems.
- Edge-profile cham de-coating for specialized corner reinforcement.
Non-Variable Specifications
- Core material density (kg/m³).
- Midnight black pigment UV-stability coefficient.
- Base structural thermal expansion coefficient (CTE).
Capacity, Tooling and Scheduling
Production timelines are dictated by the availability of specialized CNC tooling required for the split-face geometry. For orders exceeding 5,000 units, we implement a staggered manufacturing schedule to ensure the curing time of the resin-impregnated layers is not compromised by high-speed throughput demands.
Standard lead times for custom-configured exports range from 8 to 12 weeks depending on the complexity of the hardware integration. We review current factory capacity for specific project windows.
Stock Availability and Quality Control
| Usage Condition | Typical Complaint | Prevention Specification |
|---|---|---|
| High-pressure concrete pours | Panel warping or surface deflection | Cross-linked resin matrix density ratio |
| Repeated mechanical stripping | Abrasion of the black finish | Vacuum-impregnated pigment penetration depth |
| Long-term outdoor exposure | Color fading or brittleness | UV-stabilized polymer additive concentration |
Request technical datas and bulk pricing for your next project.
Contact Our Export Department for a Quotation